 Chinese
 English
 Russian
I、 Shortcomings in the working conditions of traditional hydraulic return oil filtration design
The return oil filters of traditional small construction machinery mostly only have single-stage filters installed at the oil tank return port. This structure can be maintained in clean environments and low operating intensity, but in harsh working conditions with high dust and mud, defects will be quickly exposed. During shovel loading operations, it is inevitable that trace amounts of dust will seep into the hydraulic circuit at the sealing of the pin shaft and hinge joint; The piston rod of the oil cylinder extends and retracts back and forth, and the small particles attached to the surface of the rod are carried into the hydraulic oil. There is an inherent contradiction in single-stage filters: the higher the precision of the filter screen, the easier it is to clog, causing an increase in return oil back pressure; The accuracy of the filter decreases, and small abrasive particles cannot be intercepted and will continue to circulate within the system.
The engine vibration of the fuel loader itself is large, the hydraulic oil temperature fluctuates greatly, the oil aging rate is faster, and the amount of impurities generated is higher. Although electric loaders do not have an engine vibration source, the frequency of electro-hydraulic composite actions is higher. The oil cylinder and directional valve repeatedly move. Once the oil contains hard particles, the wear rate of the components will continue to accelerate. Many user devices experience hydraulic system leakage after six months to a year of use, resulting in weak bucket lifting and slower response. Upon disassembly, it was found that there were a large amount of metal debris inside the hydraulic oil, which was caused by insufficient oil filtration capacity and the circulation of pollutants in the hydraulic circuit.
At the same time, the traditional filter clogging warning mechanism is missing. After the filter screen is clogged, the bypass valve will open directly, and unfiltered hydraulic oil will return to the oil tank directly. The operator cannot detect it at the first time, and the system continues to be contaminated. By the time the fault is discovered, irreversible damage has already occurred to the pump body and valve group. In the multi shift continuous operation factory area, once the hydraulic core components are damaged, the repair and disassembly process takes a long time, directly interrupting the material transfer rhythm of the production line and causing significant production losses.
II、 Architecture Design of Jining Xinghang Layered Return Oil Filtration System
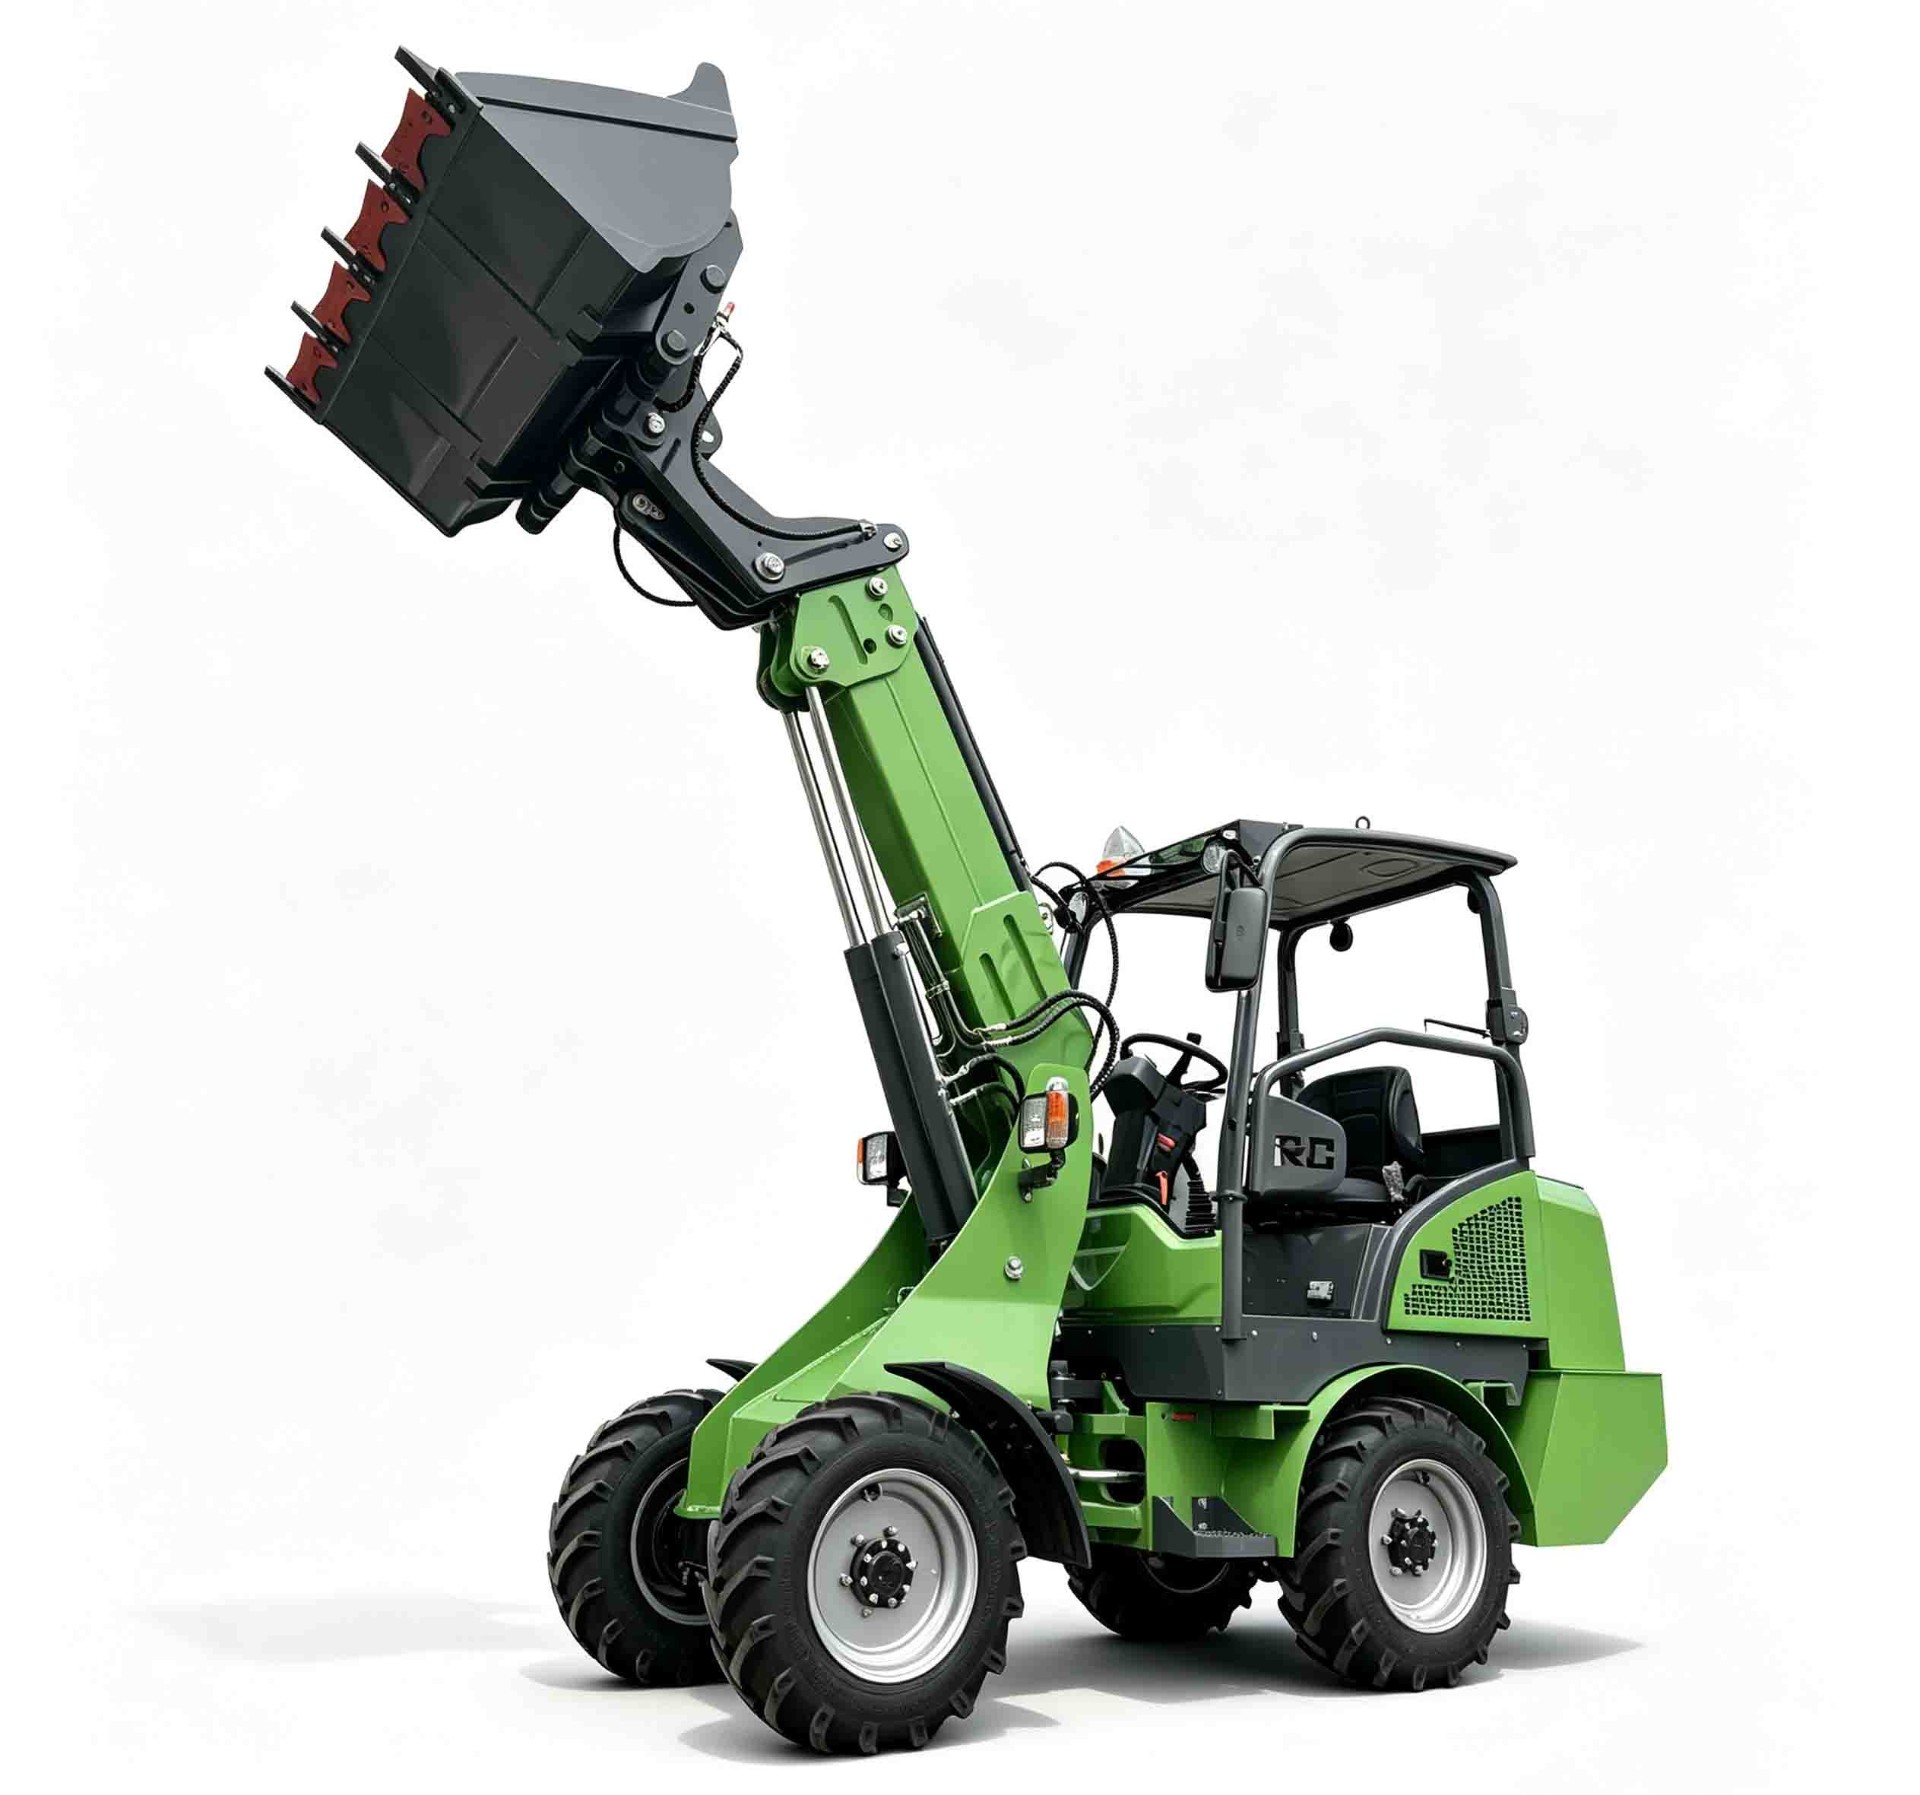
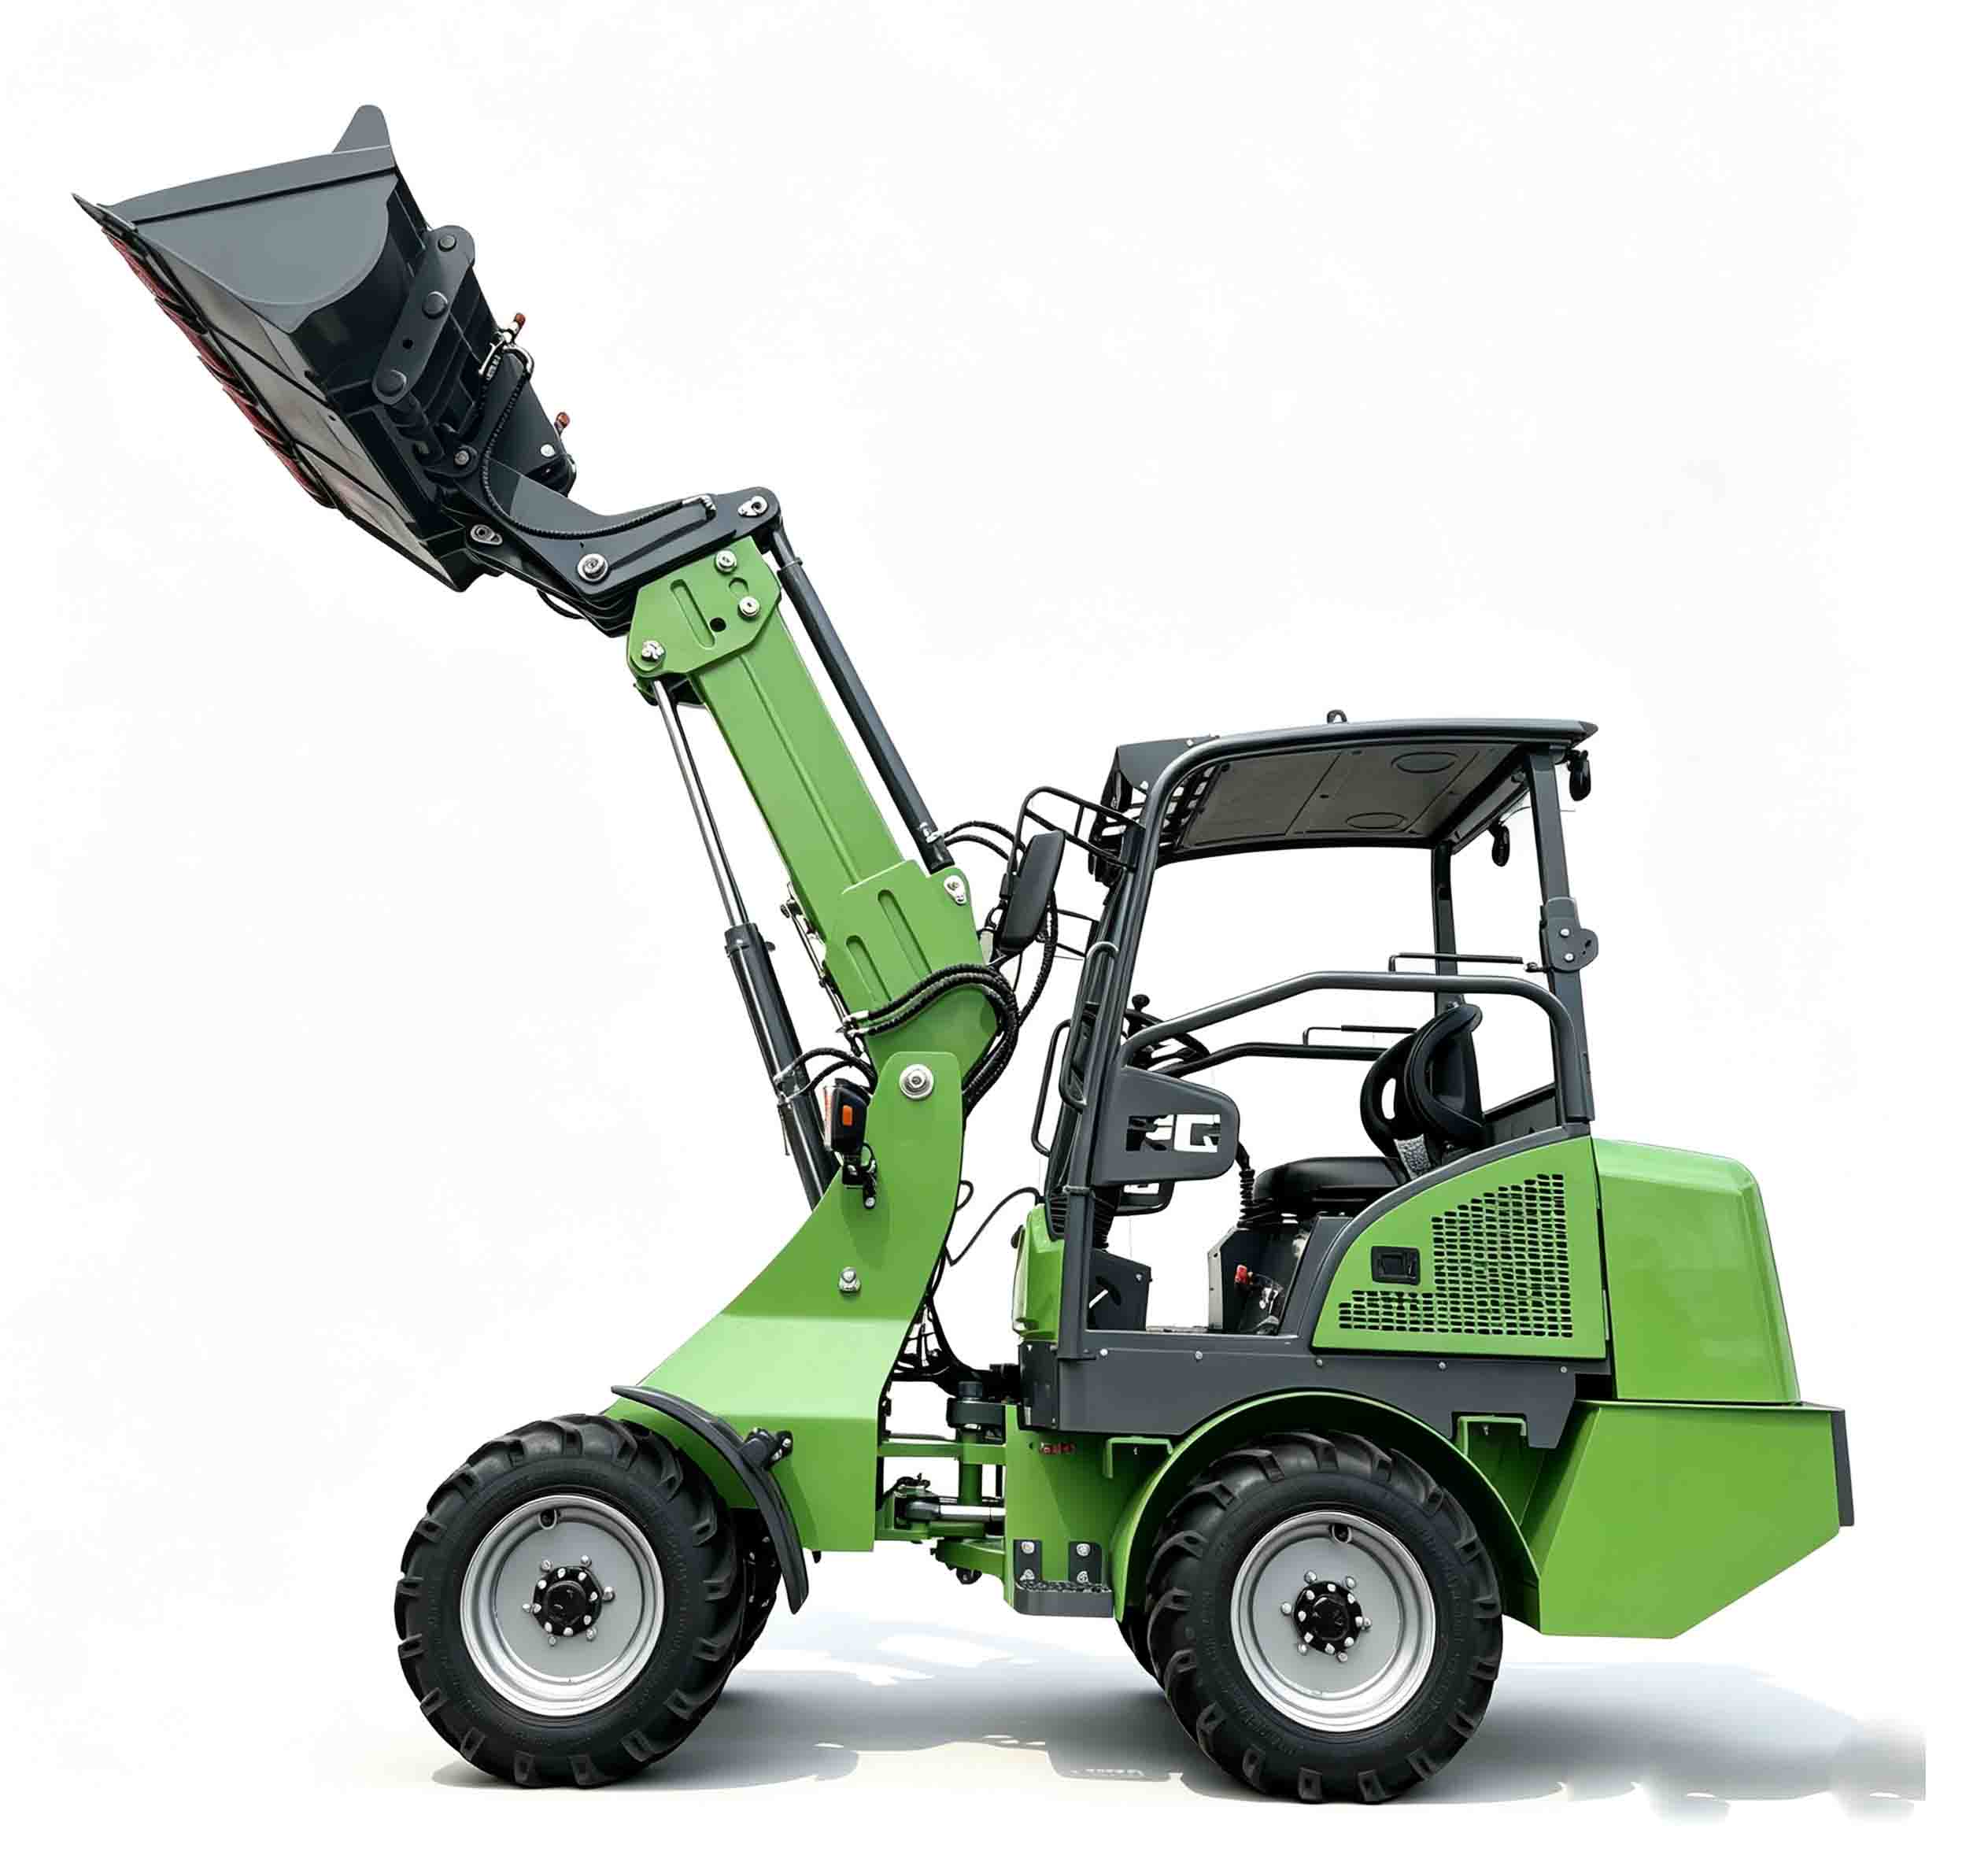
In response to the pain points of on-site working conditions, Jining Xinghang electric loader adopts an integrated oil return filtration scheme of multi-stage oil return filtration, pressure monitoring, and bypass protection, changing the protection logic of a single filter element. The entire system is divided into three levels: pre coarse filtration, main circuit fine filtration, and tank bottom sediment collection, each performing its own duties to achieve graded interception of impurities of different particle sizes.
The first level is the pre oil return coarse filter, which is arranged at the position of the oil cylinder return oil collection pipeline. It prioritizes intercepting large particles of sediment and rubber debris, avoiding direct impact of large particles on the rear fine filter element, protecting the main filter element, and extending the fine filter replacement cycle. The coarse filter element has a large dirt holding capacity, and it is not easy to quickly block the sudden influx of a large amount of impurities into the material yard.
The second level is the main return oil fine filter, which serves as the core of the entire filtration system and is responsible for intercepting micrometer sized metal abrasive particles and fine dust. The filter element is made of high-strength composite filter material, which balances filtration accuracy and oil flow capacity, reduces return oil back pressure, and avoids excessive back pressure affecting the reset action of the oil cylinder. The filter housing integrates a differential pressure sensor to monitor the pressure difference between the upstream and downstream of the filter element in real time. When the filter element is clogged and the pressure difference reaches the set threshold, a warning prompt will pop up on the dashboard of the cab, reminding the operation and maintenance personnel to replace the filter element in a timely manner, so as to avoid the problem of blind opening of the bypass valve and direct return of dirty oil to the tank. Only when the pressure difference exceeds the safety limit, the bypass valve will open for a short period of time to ensure the basic operational capability of the equipment, and at the same time, it will continuously sound an alarm to prevent pollution without warning.
The third level is the optimization of fuel tank sedimentation structure. Jining Xinghang has designed a diversion baffle inside the hydraulic oil tank. After the return oil enters the tank, the flow rate of the oil slows down, and heavy impurities settle to the sedimentation zone at the bottom of the tank by gravity. Regular oil discharge can discharge the sediment and reduce suspended particles from entering the oil suction pipeline. The fuel tank cover plate is equipped with a breathing filter device, which allows the working oil of the equipment to undergo thermal expansion and contraction. When the air inside the fuel tank is exchanged, external dust will not enter the tank with the air, reducing the entry of new pollutants into the hydraulic oil from the source.
III、 The logic of improving the service life of hydraulic components by the return oil filtration system
The wear of hydraulic components mostly belongs to abrasive wear. When the hydraulic oil maintains high cleanliness, the small gaps between the internal mating surfaces of the pump and valve will not be scratched by hard particles, and the internal leakage rate of the components will be significantly slowed down. For the multi way valve used in high-frequency electric loaders, the clearance between the valve core and the valve hole is extremely small. When small particles scratch the valve core, there will be internal leakage in the valve group and insufficient force in the composite action. A stable oil return filtration system continuously purifies the oil, protects the precision matching pair, maintains the control accuracy of the multi way valve, and improves the consistency of long-term operation actions.
Hydraulic cylinder seals also benefit. Particles in the oil will continue to scratch the piston rod seal, causing oil leakage. Clean hydraulic oil reduces seal wear and reduces external cylinder leakage faults. The entire hydraulic system maintains stable working conditions, and the rate of oil aging will also slow down, extending the hydraulic oil replacement cycle and reducing the cost of maintenance consumables in the later stage.
Unlike fuel powered models, the electronic control system of Jining Xinghang electric loader can collect filter pressure difference data and connect it to the overall fault diagnosis system. Maintenance personnel can check the status of the filter element without dismantling the pipeline during daily inspections, turning passive repair into preventive maintenance. Many equipment failures are discovered in the early stages to prevent minor issues from escalating into major failures of core hydraulic components.
IV、 Key points for on-site operation and maintenance, maximizing the value of the filtration system
Even the best hardware design needs to be coordinated with standardized operation and maintenance to fully realize its value. Firstly, the filter element must be selected from products that match the specifications, and low-priced filters with inconsistent accuracy cannot be replaced at will, otherwise it will damage the protective ability of the entire filtration system. Secondly, when replacing hydraulic oil or disassembling hydraulic pipelines, it is important to ensure proper pipe protection to prevent dust from entering the circuit on site. Oil discharge and maintenance operations should be carried out during periods of low wind and dust to minimize the entry of pollutants into the system during maintenance.
Daily inspections should focus on the differential pressure alarm prompt of the cab filter element. If there is a warning, do not continue with long-term heavy load operations and arrange for the replacement of the filter element in a timely manner. Regularly open the drain plug at the bottom of the fuel tank to remove sediment impurities and reduce the load on the filter element. Many users tend to overlook the fuel tank breathing filter. A clogged breathing filter can cause negative pressure in the fuel tank, which not only affects pump suction but also accelerates dust inhalation. It needs to be included in the regular inspection checklist.
V. Conclusion
The reliability of the hydraulic system determines the overall attendance rate of the electric loader. The layered hydraulic return oil filtration system of Jining Xinghang electric loader is not simply adding a filter, but constructing a protection plan from the entire chain of pollutant generation, invasion, and circulation. Under continuous dust conditions in the factory material yard, maintain the cleanliness of hydraulic oil, reduce abrasive wear on pumps, valves, and oil cylinders, extend the service life of hydraulic components, and reduce the frequency of shutdown maintenance. For users who pursue continuous and stable output of equipment and control long-term operation and maintenance costs, the long-term benefits brought by this oil return filtration design will continue to be reflected in the long-term service life of the equipment.